Related Topics:
Automatic Inter Cell Welding-
Welding helmet automatic light-changing battery
Not only putting a replacement takes time, it costs money too. So, you don't just want to throw a battery away when there is nothing wrong with it. But how do you find out? I'm now laying out the common steps, so you at least know how to do it. Don't worry! I'll talk about the procedures for some popular brands too. Auto-darkening helmets feature either. Miller's helmets are very popular, and so are those from other manufacturers. Some of the models require the users to remove both the inside and. I guess you've learned all I intended from this article except one thing. Auto-darkening helmets that have both solar panels and batteries are.
FAQs about Welding helmet automatic light-changing battery
Should I replace the battery in my Auto Darkening welding helmet?
With a little effort and attention to detail, replacing the battery in your auto darkening welding helmet will be a breeze. Replacing the battery of your welding helmet is an important task that you should undertake when the old battery has become ineffective.
Why do welding helmets have two batteries?
The two batteries serve two distinct purposes. The first battery is used to provide power for analog circuits that process the optimum light intensity. The second battery regulates the lens voltage, which determines the level of darkness. After you have securely installed the two batteries, you will need to put your welding helmet to the test.
Do auto-darkening welding helmets need batteries?
Most auto-darkening welding helmets are powered by batteries, which means you may have to change the batteries from time to time as they get depleted. Changing batteries is an important skill to have as a welding professional. You should be able to change the helmet's battery quickly without allowing it to affect your productivity.
How do I replace the battery on my Auto-Darkening welding helmet?
Auto-darkening welding helmets come with either removable or fixed batteries, so there are typically two approaches to replacing them. UNCLIP the main panel from the lens covers and remove it. LOCATE the battery holder/tray, referring to the user manual if needed. Carefully REMOVE the battery holder with your fingers or a pair of tweezers.
How to replace a welding helmet battery?
Replacing the battery of your welding helmet is an important task that you should undertake when the old battery has become ineffective. The first step in this process is to turn off the welding helmet to avoid electrical shock. Next, locate the battery compartment on the helmet, which is usually located on the side of the helmet.
What batteries are used in a welding helmet?
The most common welding helmet batteries are CR2450 and CR2032 coin batteries. CR2025 and CR2450 are also used in some hoods. They are typically located in a chamber adjacent to the ADF control panel and are shielded from damage during welding. Many welding helmets include a battery indicator LED to alert users when batteries are low.
-
Cylindrical battery pack automatic integrated machine
This specialized equipment is designed to automate the assembly of cylindrical battery cells into high-performance battery packs, ensuring precision, consistency, and safety in every step of the process.
-
21700 Top Ten Battery Cell Brands
Here are the top 10 21700 battery companies in the world: EVE, Sunpower, BAK, LISHEN, FESC, GREAT POWER, LG, SAMSUNG, SVOLT and SILVER SKY.
FAQs about 21700 Top Ten Battery Cell Brands
What are 21700 batteries?
21700 batteries are lithium rechargeable batteries that come in various versions with differences in battery capacity, pulse rate, drain current, charging current, and battery terminals, among other things.
What are the top cell phone battery manufacturers?
When it comes to long-term trends, this is how the leading manufacturers tend to fare. #1 Samsung Samsung can arguably be considered the top cell phone battery manufacturer globally.They produce batteries for their own phone models, and Samsung consistently pushes the boundaries of what lithium-ion technology can achieve.
How big is 21700 battery in China?
The total planned scale of 21700 will reach 7GW. At present, it has formed supporting cooperative relations with China's mainstream new energy smart car companies, and continues to expand strategic customers, emerging Internet car companies, etc. Jiangsu Zhihang in Top 10 21700 battery manufacturers in China was established in July 2012.
What is the best 21700 power cell?
The newest generation Molicel INR21700 P45B is a very good version with a 7% higher capacity and 22% lower DCR compared to P42A. Its discharging performance has been enhanced hugely with superior fast charge capability up to 3C charging rate.
Who is the best lithium ion battery manufacturer in China?
Tianjin Lishen As the No. 1 in Top 10 cylindrical lithium ion battery manufacturers was founded on December 25, 1997. It has an annual production capacity of 13G watt-hour lithium-ion batteries, and its international high-end market share ranks among the forefront of the global lithium battery industry.
Who is Tesson battery?
Tesson focuses on the technical route of the ternary system, provides power battery solutions for new energy vehicles, and provides energy storage solutions for large-scale smart energy storage power stations and backup power supplies. Now become one of Top 10 21700 battery manufacturers in China.
-
Vanadium liquid flow battery single cell voltage
Open-circuit voltage of an individual cell in the range of 1 V. 2 V Determined by the particular chemistry For higher terminal voltages, multiple cells are connected in series.
FAQs about Vanadium liquid flow battery single cell voltage
What is a vanadium flow battery?
Vanadium flow batteries employ all-vanadium electrolytes that are stored in external tanks feeding stack cells through dedicated pumps. These batteries can possess near limitless capacity, which makes them instrumental both in grid-connected applications and in remote areas.
What is a single vanadium element battery?
Their single vanadium element system avoids capacity fading caused by crossover contamination in iron-chromium flow batteries (ICFBs) . Additionally, VRFBs use an aqueous electrolyte, eliminating the safety risks associated with bromine vapor corrosion in zinc-bromine flow batteries (ZBFBs) .
What is a single cell vanadium redox flow battery (VRFB)?
A laboratory-scale single cell vanadium redox flow battery (VRFB) was constructed with an active area of 64 cm 2. The electrolyte was produced by dissolving vanadium pentoxide in sulphuric acid.
What is a vanadium redox flow battery?
Vanadium redox flow battery is one of the most promising devices for a large energy storage system to substitute the fossil fuel and nuclear energy with renewable energy. The VRFB is a complicated device that combines all the technologies of electrochemistry, mechanical engineering, polymer science, and materials science similar to the fuel cell.
What is the ideal electrolyte for vanadium batteries?
The ideal electrolyte for vanadium batteries needs to ensure the stability of high-concentration vanadium ions in different oxidation states over a wide temperature range. A key issue to be resolved is to improve the stability of V 5+ at high temperatures (50 °C) and V 3+ at low temperatures (−5 °C).
Can ion transport improve vanadium redox flow battery electrolytes?
Furthermore, research progress in other battery fields shows that optimizing electrolyte formulations [21, 22] and ion transport [23, 24] can significantly enhance energy density and cycling stability, providing valuable insights for improving vanadium redox flow battery electrolytes. Table 1.
-
What is 21700 cylindrical battery cell
The 21700 battery is a Li-ion battery named after its 21mm × 70mm cylindrical size (diameter × height). When compared to AA size and 18650 type cells, their height and diameter both are larger.
FAQs about What is 21700 cylindrical battery cell
How big is a 21700 battery?
The diameter of the 21700 battery is 21mm. To be more precise, it has an approximate length of 70mm and an approximate diameter is 21mm but technically 21700 cell size is allowed with some tolerance in length and diameter. Thus you could find specifications written as (say) 21 ± 0.41mm ✖ 70 ± 0.25mm on the datasheet and features of the li-ion cell.
What is a 21700 cell?
21700 cell, as the name suggests, stands for a cylindrical cell with 21mm width and 70mm height. It was first introduced in 2017 by a Tesla and Panasonic collaboration. 21700 was introduced as an alternative to the long-running 18650 model, which was introduced by Sony in 1991.
How big should a 21700 cell be?
The 21700 cell increased the working volume over the 18650 by a factor of >1.4x 21700 => ~21mm in diameter and ~70.0mm long These dimensions vary between manufacturers. Using data from the Cell Database we can see that 70g is a good nominal figure for the mass of a 21700 cell. The 21700 cell by definition should be 21mm in diameter and 70mm high.
Are 21700 batteries based on lithium ion?
However, most 21700 cells are based on lithium-ion (Li-ion) technology, which is widely used across many types of rechargeable batteries due to its excellent energy density and long lifespan. There are several types of lithium-ion chemistries that could be used within the 21700 format:
What is the difference between a 21700 and 18650 battery?
The most significant difference between the 21700 and 18650 batteries is their size and capacity. The 21700 is larger (21mm x 70mm) compared to the 18650 (18mm x 65mm), and this size difference allows the 21700 to store more energy. Capacity: The 21700 typically holds 5000mAh or more, while the 18650 generally maxes out around 3500mAh.
What are the advantages of 21700 batteries?
One of the key advantages of 21700 batteries is their energy density. Typically, 21700 batteries have an energy density ranging from 250 Wh/kg to 300 Wh/kg, depending on the chemistry used. This is a notable improvement compared to 18650 batteries, which usually offer around 180 Wh/kg to 250 Wh/kg.
-
Chemical formula of battery cell production process
The anode and cathode materials are mixed just prior to being delivered to the coating machine. This mixing process takes time to ensure the homogeneity of the slurry. Cathode: active material (eg NMC622), polymer binder (e.g. PVdF), solvent (e.g. NMP) and conductive additives (e.g. carbon) are batch mixed. The anode and cathodes are coated separately in a continuous coating process. The cathode (metal oxide for a lithium ion cell) is coated onto an aluminium electrode. The. The electrodes up to this point will be in standard widths up to 1.5m. This stage runs along the length of the electrodes and cuts them down in width to. Immediately after coating the electrodes are dried. This is done with convective air dryers on a continuous process. The solvents are recovered from this process. Infrared technology is used as a booster on Anode lines.
[PDF Version]
FAQs about Chemical formula of battery cell production process
What are the three steps of battery production?
Battery cell production is divided into three main steps: (i) Electrode production, (ii) cell assembly, and (iii) cell formation and finishing . While steps (1) and (2) are similar for all cell formats, cell assembly techniques differ significantly . Battery cells are the main components of a battery system for electric vehicle batteries.
How are lithium ion battery cells manufactured?
The manufacture of the lithium-ion battery cell comprises the three main process steps of electrode manufacturing, cell assembly and cell finishing. The electrode manufacturing and cell finishing process steps are largely independent of the cell type, while cell assembly distinguishes between pouch and cylindrical cells as well as prismatic cells.
What is lithium ion battery production?
lithium-ion battery production. The range stationary applications. Many national and offer a broad expertise. steps: electrode manufacturing, cell assembly and cell finishing. cells, cylindrical cells and prismatic cells. each other. The ion-conductive electrolyte fills the pores of the electrodes and the remaining space inside the cell.
What is a battery cell made of?
The cell is filled with an electrolyte, which is composed of lithiumhexafluorophosphate (LiPF6) conductive salt . The manufacturing process of the cell is the one described in . The data for the energy consumption of the battery cell manufacturing are taken from .
What is the battery manufacturing process?
The battery manufacturing process is a complex sequence of steps transforming raw materials into functional, reliable energy storage units. This guide covers the entire process, from material selection to the final product's assembly and testing.
What is the first step in the lithium battery manufacturing process?
Electrode manufacturing is the first step in the lithium battery manufacturing process. It involves mixing electrode materials, coating the slurry onto current collectors, drying the coated foils, calendaring the electrodes, and further drying and cutting the electrodes. What is cell assembly in the lithium battery manufacturing process?
-
Cylindrical lithium battery cell
The cans for the 18650 and 21700 are made from nickel plated steel and deep drawn in a two-stage process. The result is the base of the can is thicker than the cylindrical side wall. 1. 18650 1.1. Base thickness ~0.3mm 1.2. Wall thickness ~0.22 to 0.28mm 2. 21700 2.1. Base thickness ~0.3. Cylindrical cells are used in numerous applications and cooling varies from passive through to immersed dielectric cooling. The diameter, length and connection of the. Cylindrical cells are designed with a number of safety features including a defined vent path/weakness. The capacity is relatively small and.
FAQs about Cylindrical lithium battery cell
What is a cylindrical lithium battery cell?
Cylindrical lithium battery cells are generally used in power batteries, such as the typical 21700 battery cells carried in the Tesla Model 3, which once made 21700 popular in the battery cell market. However, cylindrical cells are not the only advantages; their shortcomings are also obvious.
How many Li-ion cylindrical battery cells are there?
This paper investigates 19 Li-ion cylindrical battery cells from four cell manufacturers in four formats (18650, 20700, 21700, and 4680). We aim to systematically capture the design features, such as tab design and quality parameters, such as manufacturing tolerances and generically describe cylindrical cells.
What are the different types of cylindrical lithium batteries?
There are many types of cylindrical cells, such as 14650, 17490, 18650, 21700, 26650 and so on. Cylindrical lithium batteries are more prevalent in Japanese and Korean lithium battery companies, and there are also companies of appropriate scale in China that produce cylindrical lithium batteries. Ⅲ.
How do you identify a cylindrical lithium-ion battery?
For instance, “65” represents a height of 65mm. Fifth Digit: The fifth digit indicates the cylindrical shape of the cell. Typically, it's “0” for cylindrical cells. By following this naming convention, we can easily identify the size and shape of cylindrical lithium-ion battery cells.
How to design cylindrical Li-ion battery cells?
A generic overview of designing cylindrical Li-ion battery cells. Function 1: Two types of jelly roll designs can be distinguished: With tabs and tabless. Jelly rolls with tabs can be realized with a single tab (Design A) or several tabs in a multi-tab design (Design B).
What is a cylindrical battery?
The following is a common cylindrical cell structure; see the image below for details: Ordinary cylindrical lithium-ion batteries consist of a casing, a cap, a positive electrode, a negative electrode, a separator, and an electrolyte. Generally, the battery casing is the battery's negative electrode, and the cap is the battery's positive electrode.
-
Battery welding materials
In this blog post, we'll explore the various materials used for cell-to-cell welding in battery pack assembly and provide guidance on choosing the most suitable option for your project.
FAQs about Battery welding materials
What are the different battery welding technologies?
Common battery welding technologys are: ultrasonic welding, resistance spot welding, laser welding, pulse TIG welding. This post combines the application results of the above battery welding technologies in lithium-ion battery systems, and explores the influencing factors. Ultrasonic welding is a solid state battery welding process.
How do you Weld a battery pack?
“We see a lot of laser welding and ultrasonic wedge bonding for the larger packs,” says Boyle at Amada Weld Tech. “If the packs or the overall volume are smaller, then resistance welding is often used. Micro-TIG comes up for specialised battery packs with low-volume production.
How are battery cells welded?
Different welding processes are used depending on the design and requirements of each battery pack or module. Joints are also made to join the internal anode and cathode foils of battery cells, with ultrasonic welding (UW) being the preferred method for pouch cells.
What types of welding do EV batteries need?
“In these situations, cooperative development and reliable relationships are of high value.” While there many kinds of welding, in EV battery applications the most common are resistance welding and laser welding, along with ultrasonic welding and wire bonding, and benefit from standardisation for mass production.
Which welding techniques can be used for connecting battery cells?
Brass (CuZn37) test samples are used for the quantitative comparison of the welding techniques, as this metal can be processed by all three welding techniques. At the end of the presented work, the suitability of resistance spot, ultrasonic and laser beam welding for connecting battery cells is evaluated.
Can a battery be welded?
There are only so many ways to join materials together, and for battery applications – particularly where high currents and voltages and tough operating environments are encountered – welding beats alternatives such as soldering, conductive adhesives and mechanical fasteners.
-
Battery Cell Production Supervisor Job Functions
Production Supervisor, Battery Cell ManufacturingLead and develop a motivated production teamCollaborate with engineering to enhance manufacturability and productivityDevelop training programs and support team member growthOversee issue resolution and maintain quality standardsDevelop and uphold standardized Manufacturing InstructionsEnsure safety and compliance, promoting continuous improvement.
-
Fully automatic lead-acid battery cabinet production line
The automatic lead-acid battery assembly line is an efficient and precise battery production equipment designed for the assembly, welding, liquid filling, and sealing processes of lead-acid batteries.
FAQs about Fully automatic lead-acid battery cabinet production line
Where can I find the lead acid battery production model tutorial?
The tutorial teaches how to: You can find the Lead Acid Battery Production Model tutorial in the Tutorials section of AnyLogic Help. To find it, you will need AnyLogic 8.5 or access to the online AnyLogic Help. We recommend the tutorial for everyone who models in AnyLogic, even if you are already familiar with the Material Handling Library.
What equipment is used in automotive battery production?
Our automotive lead-acid battery production equipment includes enveloping/wrapping & stacking machines, an element check and buffer system, cast-on-strap machines and full assembly lines. Did you know that the annual demand for automotive batteries is approx. 400 million pieces worldwide?
What is automotive lead-acid battery technology?
Our technology is used to produce telecom preforms, specialty preforms and fibers. The automotive lead-acid battery sector covers all SLI (starting, lighting, ignition) batteries. This includes the following technologies: With our complete assembly solutions for car and truck batteries, we have the expertise to fulfil your needs.
Are automotive battery assembly lines reliable?
As with any mature technology, battery manufacturers expect an automotive battery assembly line to be highly dependable and work on an almost nonstop basis.
When was the first rechargeable lead-acid battery invented?
The first practical version of a rechargeable lead-acid battery was invented in 1859. Of course, the technical requirements have changed enormously since then. We are all the more pleased that we have been supplying the lead-acid battery manufacturing sector with our production equipment for more than 50 years now.
What is automotive battery assembly equipment?
Our assembly equipment handles automotive battery applications from car to truck and covers all SLI (starting, lighting, ignition) batteries.
-
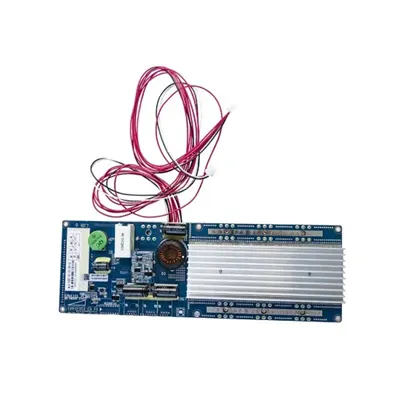
Automatic voltage boost for lithium battery pack
Lithium-ion batteries are becoming increasingly popular for energy storage in various hybrid energy systems, hybrid ac/dc, micro-grid, e-mobility applications. However, due to the wide battery impedance ran.
FAQs about Automatic voltage boost for lithium battery pack
Can a lithium-ion battery interfacing boost converter operate in input-voltage-controlled mode?
Small-signal model of boost converter has been derived and analyzed, when it operating in the input-voltage-controlled mode. New experimental prototype and verify method for the lithium-ion battery interfacing boost converter are built and tested.
Do AA batteries need a boost converter?
from a single AA battery), while the back-end IC or subsidiary circuit requires a higher input voltage. Therefore, a boost converter is required to convert the battery's low voltage to a higher voltage. MPS offers a large portfolio of boost converters for battery-powered applications.
How does a boost converter work?
Meanwhile, the boost converter control the input voltage, to satisfy the need of voltage regulation, based on the need of extend battery lifetime, economic optimization, and so on. During the experiment, a commercial lithium-ion battery pack has been used.
Is there a fast active cell balancing circuit for lithium-ion battery packs?
This article proposes a fast active cell balancing circuit for lithium-ion battery packs. The proposed architecture incorporates a modified non-inverting buck-boost converter to improve balancing efficiency, an equivalent circuit model technique for battery designing, and an extended Kalman Bucy filter for accurate SOC estimation.
What is the 16-cell lithium-ion battery active balance reference design?
The 16-Cell Lithium-Ion Battery Active Balance Reference Design describes a complete solution for high current balancing in battery stacks used for high voltage applications like xEV vehicles and energy storage systems.
What is virtual impedance in lithium-ion battery interfacing boost converter controller?
As the virtual impedance concept is increasingly used for the control of power electronic systems, this letter introduces virtual impedance into the Lithium-ion Battery interfacing boost converter controller, to reduce the impact of variable inner impedance.